How to Compare Custom Metal Craft Manufacturers in 2026?

Time:2026-10-21 Author:Mason
0%

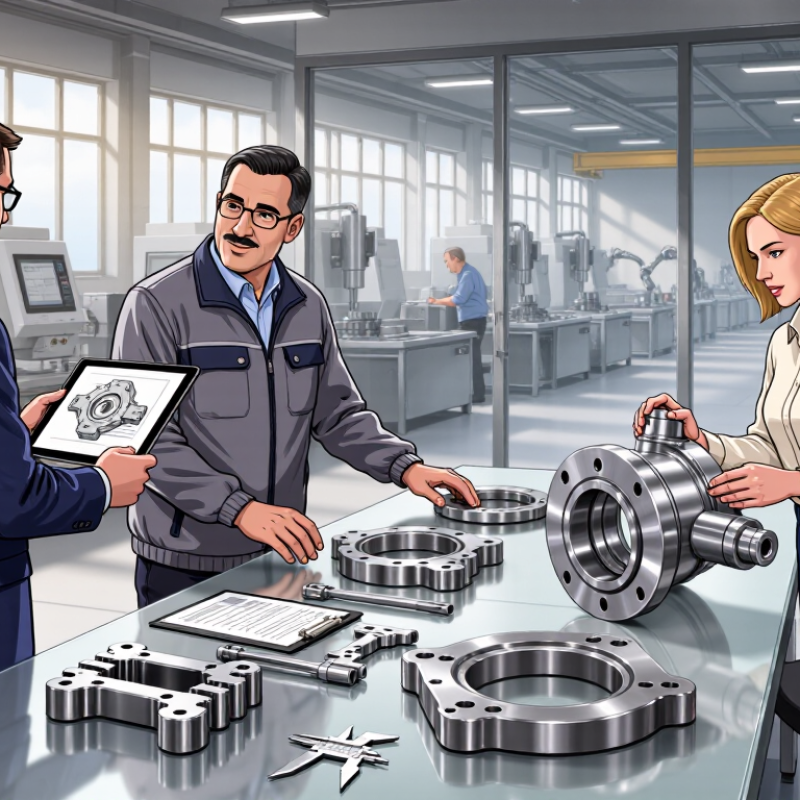
Choosing a custom metal craft manufacturer in 2026 requires more than comparing attractive product photos. It demands evidence, practical questions, and careful observation. The right partner must understand your drawings, material requirements, surface finishes, tolerances, packaging needs, and delivery schedule. A polished website proves very little. A marked sample tells you more.

This guide explains How to compare different manufacturers of custom metal crafts through measurable criteria. Review their equipment, inspection methods, production experience, and ability to handle small or changing orders. Ask for material certificates, finished samples, dimensional reports, and references from comparable projects. Examine welds, edges, coatings, engraving depth, and protective packaging. Small defects often become expensive problems later.

Paul Akers, a respected lean-manufacturing educator, says, “The best way to improve is to make small, incremental changes every day.” His principle applies to supplier evaluation. Compare how manufacturers document corrections, improve processes, and respond when something goes wrong. Their first quotation may not reveal their real capability. Their response to a difficult question often does.

No scorecard is perfect. I have seen low-cost suppliers deliver excellent prototypes, and premium suppliers miss simple deadlines. That is why evidence should outweigh assumptions. Consider total value, not only unit price. Include tooling, revisions, freight, inspection, and communication time. A reliable manufacturer should make uncertainty visible, even when the answer is inconvenient. That honesty may protect your project better than a confident promise.
How to Compare Custom Metal Craft Manufacturers in 2026?

Define Material Needs with ASTM Grades and ISO 12944 Corrosion Classes

How to Compare Custom Metal Craft Manufacturers in 2026?

Material selection should begin with the service environment, not a supplier’s catalog. ASTM grades define chemistry, strength, thickness, and fabrication expectations. For example, ASTM A36 may suit general structures, while higher-strength grades can reduce weight. Stainless steel grades require different welding and finishing controls. Ask each manufacturer for mill certificates, heat numbers, and traceable inspection records. A polished sample proves little without documentation.

ISO 12944 adds the corrosion perspective. Classify exposure from C1 to CX, considering humidity, salt, chemicals, and immersion. Then review the proposed coating system and durability range. “High durability” does not mean zero maintenance. Surface preparation, edge treatment, film thickness, and workshop climate can change the result. I have seen strong specifications fail because sharp corners received thin coating.

Tips: Give manufacturers the exact location, operating temperature, cleaning chemicals, and expected service life. Request coating inspection reports, adhesion results, and repair procedures. Compare evidence, not confident promises. Do not accept “marine grade” without a defined ISO 12944 category.

A reliable comparison also examines welding qualifications, dimensional control, packaging, and corrective-action records. Ask how the supplier handles concealed rust, distorted panels, or coating damage during transport. Their answer reveals practical experience. One detail is often overlooked: ASTM compliance and ISO 12944 compliance address different risks. They must work together. My own view is cautious; a technically correct specification can still fail when site conditions are guessed.

Audit Quality: Check ISO 9001, Traceability, and First-Pass Yield Data

When comparing custom metal craft manufacturers in 2026, audit their quality system beyond a polished factory tour. ISO 9001 certification is useful, but the certificate should match current operations. Check its validity, scope, issuing body, and covered production sites. Ask how operators handle nonconforming parts, corrective actions, and process changes. A real system leaves records.

Traceability should reach the material batch, machine, operator, and inspection result. Request a sample traveler for one finished component. It should connect the purchase order to mill certificates, forming records, surface treatment, and final measurements. Confirm that digital records cannot be casually overwritten. Small gaps matter. One missing heat number can complicate a recall or root-cause investigation.

First-pass yield data reveals process stability more clearly than impressive samples. Ask for monthly figures by process, not only an annual average. Clarify whether rework, sorting, and customer returns are excluded. Compare yield for products similar to yours, including tight bends, thin walls, or visible finishes. During audits, I have found that excellent averages can hide one troubled production cell. That deserves questions, not immediate rejection. A lower yield may reflect honest reporting, while an unusually perfect figure may need verification. Review control charts, inspection photos, and recent corrective-action reports together. Then compare the evidence with your drawings, tolerance requirements, and delivery risks.

Compare Precision: Test ±0.05 mm Tolerances and Ra 1.6 μm Finishes

How to Compare Custom Metal Craft Manufacturers in 2026?

A drawing alone cannot prove precision. Ask each manufacturer to machine the same test coupon. Specify ±0.05 mm tolerances and an Ra 1.6 μm finish. Require dimensional reports linked to calibrated equipment. ISO 286-1 provides the framework for tolerance interpretation, while ISO 21920-1 guides surface-texture measurement. These standards reduce arguments over vague terms like “high precision.”

Inspect the measurement method, not only the final numbers. A coordinate measuring machine can verify hole locations, but roughness needs a suitable stylus or optical instrument. NIST Technical Note 1297 explains that expanded uncertainty often uses coverage factor k=2, representing approximately 95% coverage. Therefore, a reported 0.05 mm result without uncertainty may look stronger than it is. Ask whether the supplier separates machine capability from inspection variation.

Look for process evidence. Industry statistical process control guidance commonly treats Cpk 1.33 as a practical capability benchmark for stable production. Request Cpk data from similar alloys, sizes, and cutting conditions. One perfect sample proves little. In supplier audits, I would also inspect burrs under angled light, measure three locations on each surface, and repeat the test after tool wear. The comparison is imperfect, but useful. A polished sample can hide unstable production. Ask what happens on the tenth batch, not only the first.

Verify Capacity Against World Steel’s 1.88 Bt 2024 Output Benchmark

The 1.88 billion tonne global crude steel output reported for 2024 offers useful context when comparing custom metal craft manufacturers. It is not a direct capacity target for one workshop. Instead, it shows the scale of the market and the pressure on supply chains.

A reliable comparison needs evidence beyond a website claim. Request monthly production records, machine lists, shift patterns, and recent delivery data. Check whether the facility owns suitable laser cutters, press brakes, welding stations, and finishing equipment. During a site visit, observe material storage, safety controls, inspection points, and unfinished orders. A large factory may still struggle with small, detailed work. A smaller shop may provide better control, but limited capacity can create delays. I have found that stated capacity often assumes perfect utilization. That assumption deserves questioning.

Tips: Compare available capacity, not total equipment capacity. Ask for output by month and product type. Review sample inspection reports and corrective-action records. Confirm steel grades, thickness tolerances, surface requirements, and packaging methods in writing. Speak with recent customers when possible. Their experience may reveal communication gaps that documents miss. Keep a small pilot order before committing to larger production. Mistakes can happen, even in well-managed facilities. Look for how openly the manufacturer explains them.

Score Sustainability Using IEA’s 7–9% Steel-Emissions Benchmark

When comparing custom metal craft manufacturers in 2026, score emissions before judging finishes or delivery speed. Use a 7–9% annual steel-emissions reduction target as a practical screening benchmark linked to IEA transition pathways. However, confirm the boundary. The figure may cover direct production emissions, purchased electricity, or the full product lifecycle.

Ask each manufacturer for verified carbon data per tonne of steel. Request electricity sources, recycled content, furnace technology, and transport assumptions. The World Steel Association reports that steel production creates roughly 7–9% of global carbon dioxide emissions, making material selection critical. A supplier using 80% recycled steel may still perform poorly if its electricity comes from carbon-intensive generation.

Keep the scoring visible.

Award points for third-party assurance, plant-level energy records, and product-specific declarations. ISO 14067 can support product carbon-footprint reviews, while ISO 14025 environmental declarations improve comparison quality. Check whether certificates cover the actual workshop, not only a parent company. Scrutinize vague claims like “green steel” without mass-balance evidence.

A simple score can assign 40% to verified emissions reduction, 25% to recycled content, 20% to renewable electricity, and 15% to reporting quality. I would not treat this weighting as perfect. Small workshops may lack expensive certification, yet provide honest production records. Ask for photographs of scrap storage, meter readings, and recent delivery documents. Evidence matters more than polished promises.

How to Compare Custom Metal Craft Manufacturers in 2026?

Score Sustainability Using IEA’s 7–9% Steel-Emissions Benchmark

Use each manufacturer’s verified cradle-to-gate steel footprint as the comparison value. Lower emissions indicate a more efficient production route. The IEA benchmark shown below represents the approximate annual emissions-reduction pace required for the steel sector to align with a net-zero pathway by 2050.

Reference ranges are indicative pathway values synthesized from IEA and worldsteel publications. Actual results vary by electricity mix, raw materials, process efficiency, and product boundary.

FAQS

How should a manufacturer’s quality certification be checked?

Verify its validity, scope, issuing body, and covered production sites. The certificate should match current operations. Ask for records showing nonconforming parts, corrective actions, and process changes. A polished factory tour proves little.

What should a reliable traceability system connect?

It should connect each component to its material batch, machine, operator, and inspection result. Request one finished-part traveler. It should link the purchase order, mill certificates, forming records, surface treatment, and final measurements. One missing heat number can complicate investigations.

Can digital production records be trusted automatically?

No. Ask how records are protected from casual overwriting. Look for revision history, approval controls, and preserved inspection results. Small gaps matter. A digital system can still contain weak evidence.

Why is first-pass yield useful during supplier evaluation?

First-pass yield shows process stability before rework or sorting. Request monthly figures by process, not only annual averages. Clarify whether rework, sorting, and customer returns are excluded. An unusually perfect figure deserves verification.

Should a lower first-pass yield immediately reject a manufacturer?

Not necessarily. Lower results may reflect honest reporting. Compare yields for similar products and difficult features, including thin walls or tight bends. One troubled production cell may distort the average. That deserves questions, not instant rejection.

How can machining precision be compared fairly?

Give each manufacturer the same test coupon and identical drawing requirements. Specify ±0.05 mm tolerances and an Ra 1.6 μm surface finish. Require dimensional reports linked to calibrated equipment. One excellent sample proves little.

What measurement evidence should accompany reported dimensions?

Inspect the measurement method, not only the reported numbers. Hole locations may require a coordinate measuring machine. Surface roughness needs a suitable stylus or optical instrument. Ask whether measurement uncertainty is reported.

What process capability information should be requested?

Request Cpk data from similar alloys, sizes, and cutting conditions. A Cpk of 1.33 is often used as a practical stability benchmark. Review control charts, inspection photos, and corrective-action reports together. The comparison is imperfect, but useful.

What should an audit examine beyond the first sample?

Inspect burrs under angled light and measure several locations on each surface. Repeat testing after tool wear. Ask what happens during the tenth batch, not only the first. The first sample can look unusually polished.

Conclusion

When learning How to compare different manufacturers of custom metal crafts, begin by defining your technical requirements clearly. Specify suitable materials through ASTM grades, then identify the required ISO 12944 corrosion-protection class according to the product’s environment. Evaluate each manufacturer’s quality system by reviewing ISO 9001 certification, material and process traceability, inspection records, and first-pass yield data. These details reveal whether a supplier can deliver consistent results rather than relying only on attractive samples or low quotations.

Precision and production capability should also be tested objectively. Request evidence that the manufacturer can maintain tolerances of ±0.05 mm and achieve surface finishes around Ra 1.6 μm when required. Compare equipment, inspection methods, lead times, and available capacity against the broader steel-production context, including the 1.88 billion-ton 2024 output benchmark. Finally, assess sustainability through energy use, emissions reporting, recycling practices, and progress toward reducing steel-related emissions in line with the 7–9% benchmark. A balanced scorecard helps identify the most reliable long-term partner.
Mason

Mason

Mason is a seasoned marketing professional with a deep expertise in the company's offerings and a passion for driving brand awareness. With a strong background in digital marketing strategies, he has an innate ability to connect with diverse audiences and effectively communicate product benefits.......